Need Help Choosing the Right Compressor? Speak to an Expert
Need Help Choosing the Right Compressor? Speak to an Expert
Need Help Choosing the Right Compressor? Speak to an Expert

Air Compressor Maintenance Guide & Checklist
An air compressor is a workhorse in any shop, garage, or industrial plant—but like any machine, it needs regular care to avoid breakdowns, costly repairs, and safety risks. A well-maintained unit lasts longer, runs more efficiently, and holds consistent pressure.
Below is the complete maintenance cycle—daily, weekly, hourly-interval, monthly, and annual tasks—plus dedicated programs for rotary screw, scroll, high-pressure paintball/PCP, and engine-driven units, including models such as HPDMC's industrial and diving air compressors. Follow it and you add 5–10 years of service life.
1. Master Maintenance Checklist (Daily to Annual)
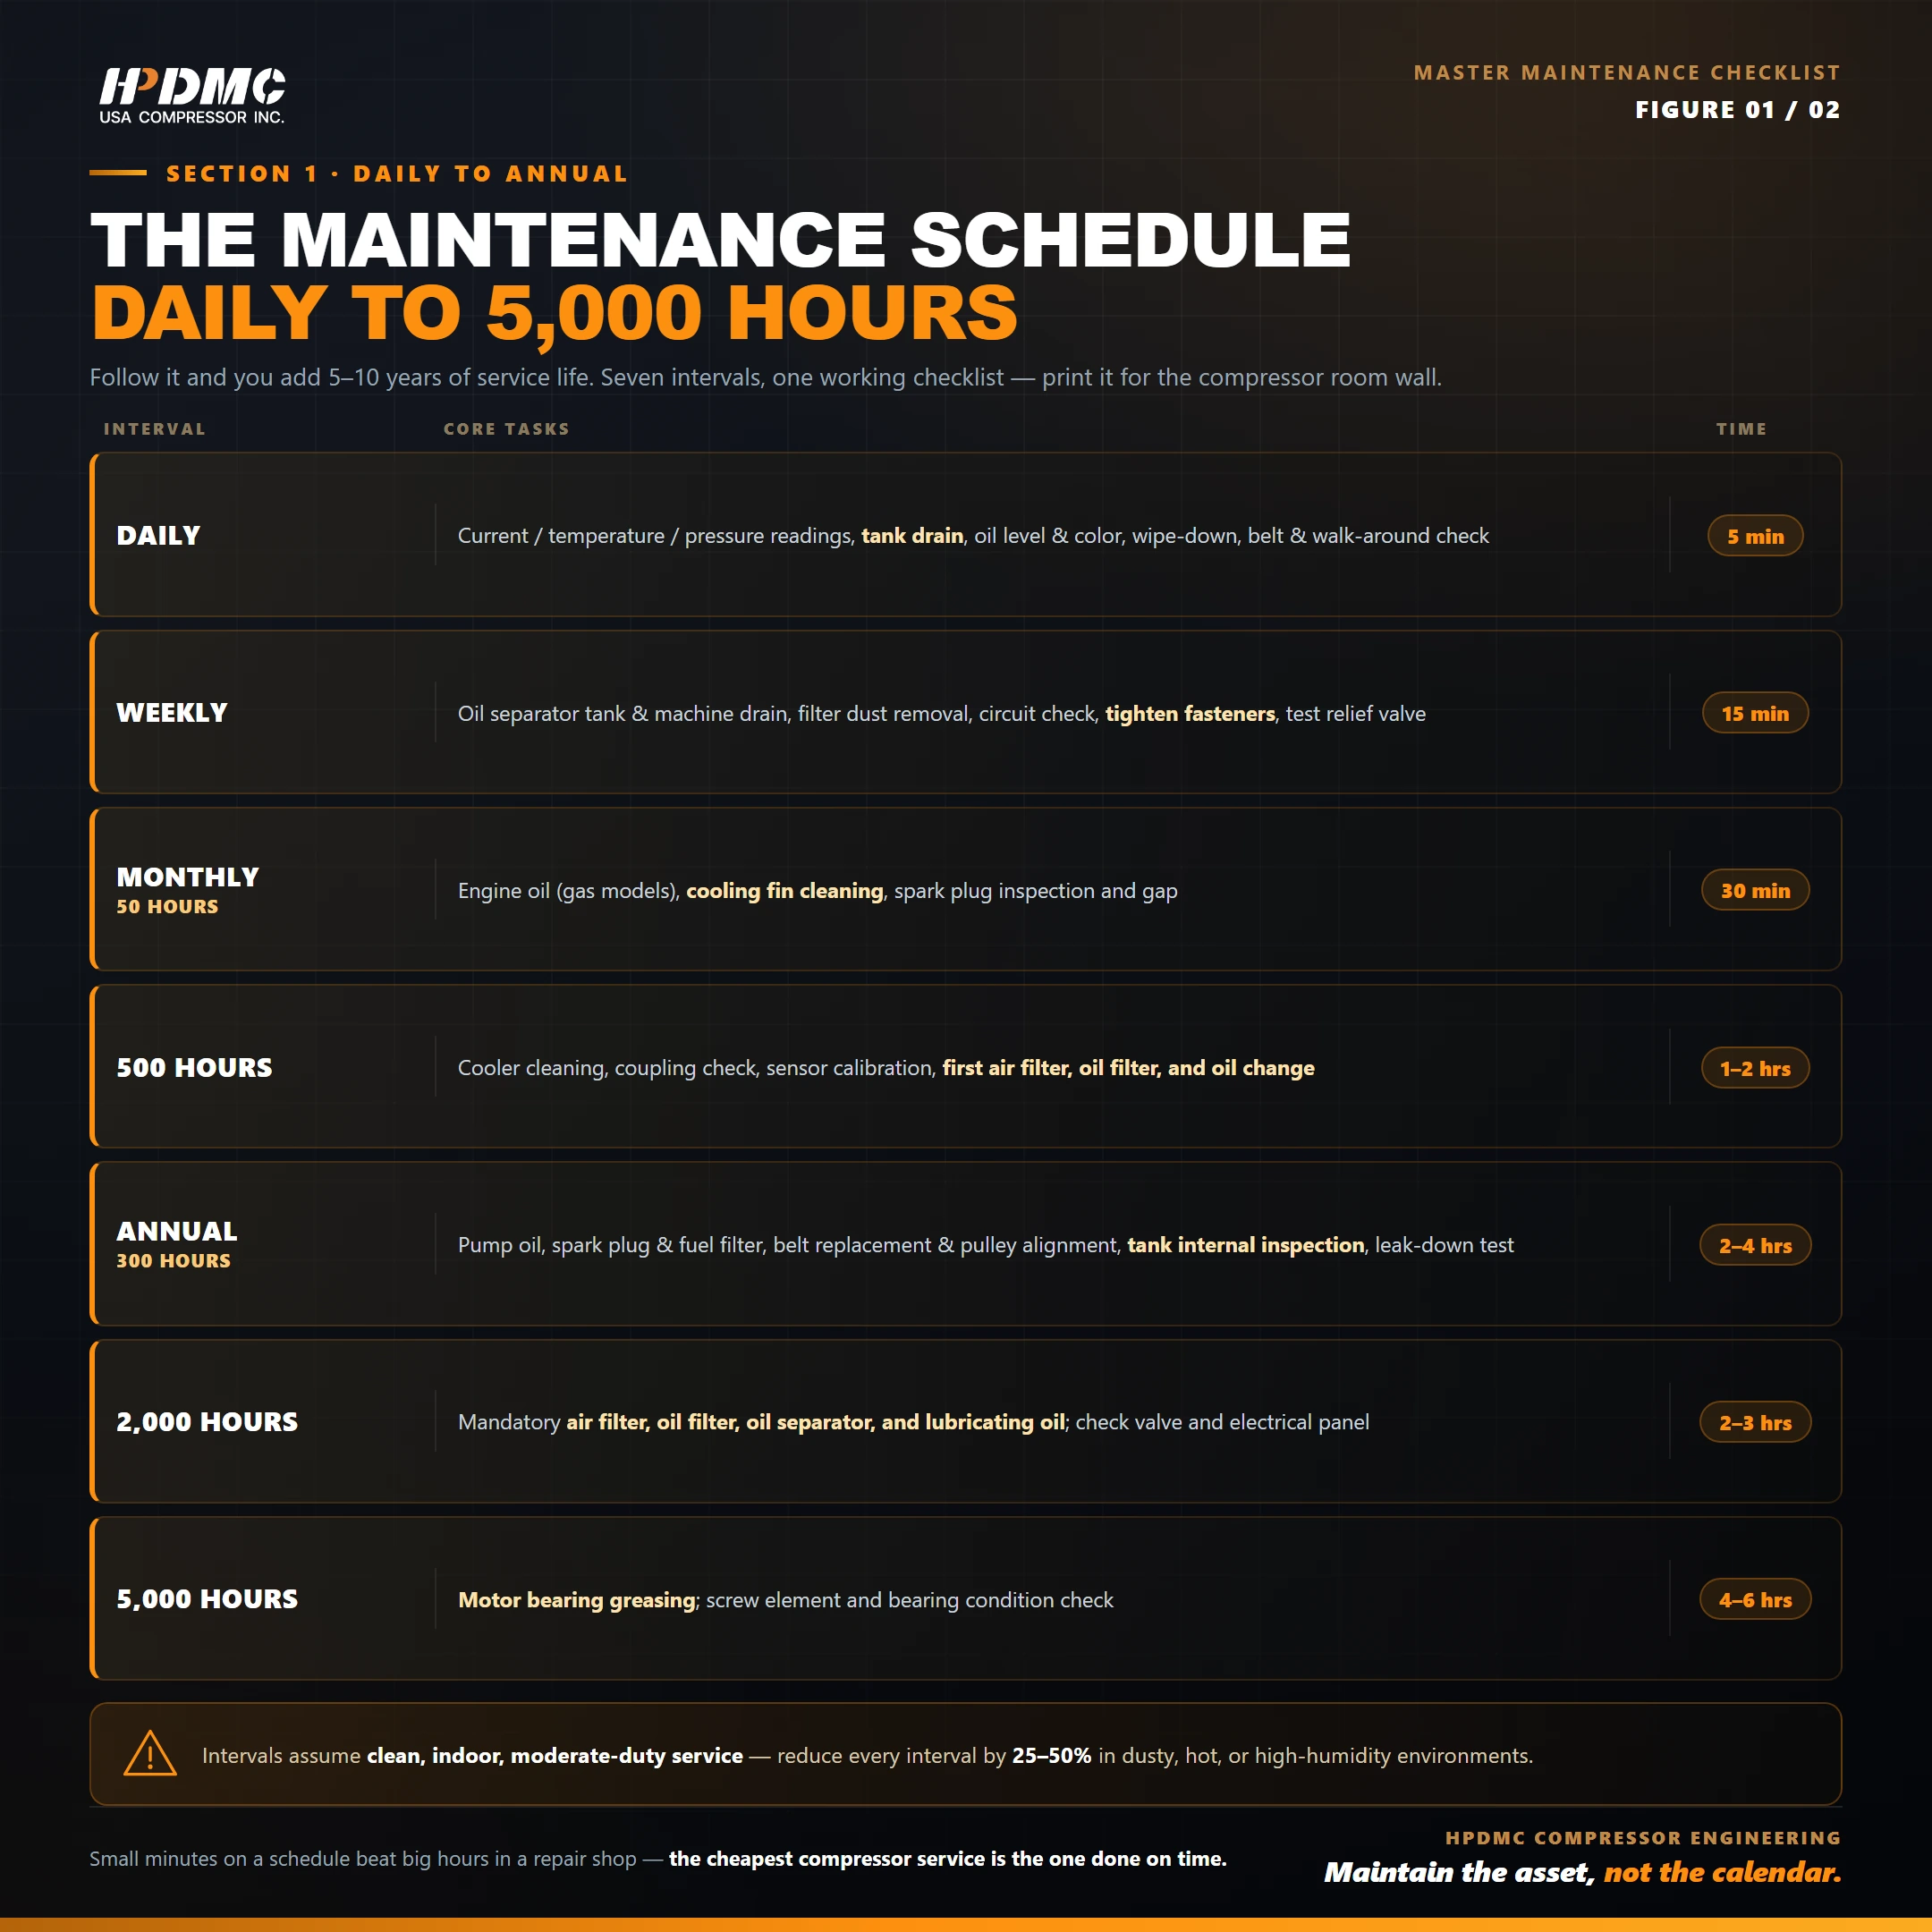
Use this table as the working checklist. Intervals assume clean, indoor, moderate-duty service—reduce every interval by 25–50% in dusty, hot, or high-humidity environments.
| Interval | Core tasks | Time |
|---|---|---|
| Daily | Current/temperature/pressure readings, tank drain, oil level and color, wipe-down, belt and walk-around check | 5 min |
| Weekly | Oil separator tank and machine drain, filter dust removal, circuit check, tighten fasteners, test relief valve | 15 min |
| Monthly / 50 hours | Engine oil (gas models), cooling fin cleaning, spark plug inspection and gap | 30 min |
| Every 500 hours | Cooler cleaning, coupling check, sensor calibration, first air filter, oil filter, and oil change | 1–2 hrs |
| Annual / 300 hours | Pump oil, spark plug and fuel filter, belt replacement and pulley alignment, tank internal inspection, leak-down test | 2–4 hrs |
| Every 2,000 hours | Mandatory air filter, oil filter, oil separator, and lubricating oil; check valve and electrical panel | 2–3 hrs |
| Every 5,000 hours | Motor bearing greasing; screw element and bearing condition check | 4–6 hrs |
2. Daily Maintenance: 5-Minute Checks
- Gauge readings. Record current, temperature, and pressure at the control panel. Abnormal values signal electrical trouble, overheating, or pressure irregularity—a sudden temperature spike usually means a cooling fault.
- Tank drain. Open the valve to release condensation. Water rusts the shell from the inside, shrinks usable volume, and carries into tools.
- Oil level and color. Check the dipstick or sight glass on lubricated models and the air tank level indicator. Clear to light amber is healthy; dark brown or black means the oil is due; milky or gray means water contamination—stop and change it now. Fill to the full mark only: overfilling foams oil into the air lines.
- Housekeeping. Wipe off dust, dirt, and spilled fluids so leaks and loose parts show up, then walk around the machine: oil drips, loose fasteners, pinched hoses—anything different from yesterday.
- Belts (machine OFF). Look for cracks, fraying, glazing, or uneven wear; deflection midway between pulleys should be about 1/2" under thumb pressure. A thrown belt stops the compressor; a slipping belt drops pump RPM and overheats belt and pulleys.
3. Weekly Maintenance: 15-Minute Tasks
Oil separator tank and machine drain. Clean both and confirm free drainage; a clog pushes oil where it should not go.
- Filter dust removal. Blow or wash the intake element and dry it fully before reinstalling. A restricted filter raises energy use and pulls abrasive dust into the pump.
- Fasteners. Vibration works bolts loose: check pump and motor/engine mounts, belt guards, pulley set screws, and tank mounts, torquing critical fasteners to spec.
- Safety relief valve. With the tank pressurized, pull the ring: it should vent freely and reseat cleanly. If it sticks, fails to release, or seeps afterward, replace it at once. This $15 valve is your only over-pressure protection—never plug or adjust it.
- Electrical connections (electric models). Power disconnected, pressure switch cover open: check terminals for tightness, corrosion, and heat discoloration, since loose connections cause voltage drop and resistance heating that kill switches and motors.
- Fuel system (gas models). Inspect lines for cracks or soft spots and the filter for sediment; clear the tank cap vent, since a blocked vent starves the engine.
4. Per 500 Hours of Operation
Cooler cleaning. Use compressed air, a soft brush, or a suitable coil cleaner. A fouled cooler cannot reject heat, and sustained heat is the top killer of components.
Coupling. Inspect for wear, damage, and misalignment; the coupling joins motor to pump, and a bad one brings vibration.
Temperature and pressure sensors. Calibrate both—bad readings invite over-pressurization or failure to shut down on high heat.
First filter and oil service. Replace the air filter and the oil filter now saturated with debris, and drain and refill lubricating oil to specification.
5. Per 2,000 Hours of Operation
📌Check valve. Inspect industrial air compressor check valves for leaks and wear; a stuck valve lets air bleed back into the pump, wasting energy and damaging it.
📌Electrical panel. Open it and inspect wiring, breakers, and components for wear, overheating, and loose terminations.
📌Mandatory replacements. Every filtration item has reached end of life: OEM replacement intake air filters restore rated airflow; high-efficiency oil separator elements stop oil carryover into dryers, tools, and processes; heavy-duty lubricant oil filters keep clean oil circulating; and synthetic rotary screw compressor oil restores lubrication and cooling, and replacement filter kits for the PACK11 and PACK15 series bundle these consumables for those models in one order.
6. Per 5,000 Hours of Operation
Grease the motor bearings to the manufacturer's quantity specification; the original grease has broken down by now. On rotary screw machines, inspect screw elements and bearing condition at this interval.
7. Monthly / 50-Hour Maintenance
➡️Engine oil (gas compressors). Change every 50 hours or monthly, whichever comes first, with SAE 10W-30 above 0°F or 5W-30 below. Kohler and Lonxin engines take roughly 1.1 quarts. Run 5 minutes before draining so warm oil carries contaminants in suspension.
➡️Cooling fins. Blow dust from engine and pump fins; clogged fins raise operating temperature and accelerate oil breakdown.
➡️Spark plug. Read the electrode: tan or light brown is healthy, black and sooty is a rich mixture, white or blistered means lean or overheating. Gap typically 0.028–0.031" for Kohler Command PRO.
8. Annual / 300-Hour Maintenance
Pump oil. Use non-detergent mineral piston air compressor oil in 4L (ISO 100 or SAE 30 in most climates) and drain while warm. On HPDMC cast-iron pumps the drain plug sits at the lowest point of the crankcase; refill to the sight glass or dipstick mark, about 16–24 oz by model. See the complete oil guide. Never use automotive engine oil in a pump—its detergents bake into carbon on valves, causing sticking and failure.
Spark plug and fuel filter (gas models). Replace both at 300 hours, or sooner if the filter is visibly loaded, using OEM or equivalent parts.
Belts and pulley alignment. Replace cracked, glazed, or unevenly worn belts and check pulley faces with a straightedge; misalignment chews belts and unevenly loads pump and motor bearings.
Tank internal inspection. On commercial units, remove the largest accessible fitting and borescope the interior for pitting at the bottom, documenting findings for insurance and regulatory records.
Leak-down test. Charge to cut-out pressure, close the outlet, stop the compressor, and time a 10 PSI drop. A tight system takes 30+ minutes; faster means leaks—find them with soapy water on every fitting, joint, and the drain.
9. Model-Specific Tips
Industrial rotary screw compressors (e.g., HPDMC 50HP): prioritize quarterly oil analysis and VSD calibration, and inspect screw elements at the 2,000- and 5,000-hour checks.
Diving air compressors: test air purity for CO, oil, and moisture monthly per EN 12021 and service coalescing filters every 50 hours.
Portable compressors: check tire pressure on wheeled units, inspect fuel lines for cracks, and monitor battery health weekly on electric models. For home and small-shop duty, see our earlier best 30-gallon air compressor picks.
10. Rotary Screw Air Compressor Maintenance
A rotary screw machine differs fundamentally from the piston compressors that dominate small shops. The airend—two precision-machined intermeshing rotors—runs at tolerances of thousandths of an inch at 3,000–6,000 RPM, and its oil is lubricant, coolant, sealant, and wear-particle transport at once, circulating at 175–200°F. Procedures that suit a piston unit destroy a screw compressor: wrong oil, a neglected separator, or a skipped inlet filter ends in airend failure—a $3,000–$15,000 repair. See our core components analysis.
Rotary Screw Oil Is Not Piston Compressor Oil
A piston compressor keeps oil in a sump, apart from the chamber; a screw compressor injects it into the chamber to lubricate rotor contacts, absorb compression heat, and seal rotor-to-housing clearances. That triple duty demands high-temperature viscosity stability, anti-foaming and oxidation additives, and demulsibility so water drops out in the separator tank. Piston oil has none of it: it foams and starves the airend, breaks down thermally, and emulsifies water into corrosion. Use only manufacturer-specified rotary screw oil—ISO VG 32, 46, or 68 by ambient and model—at $30–$60 a gallon against a rebuild.
Rotary Screw Maintenance Schedule
| Interval | Task | Estimated Time |
|---|---|---|
| Daily | Oil level, condensate drain, noise and vibration check, verify temperature and pressure | 5 min |
| Weekly | Inspect air filter, belt tension, hose and fitting leaks, clean cooler fins | 10 min |
| 500 hours | Oil sample analysis, clean or replace air filter, inspect electrical connections | 15 min |
| 2,000 hours | Change oil and oil filter, replace air filter | 1 hr |
| 4,000 hours | Oil, oil filter, air filter, and air/oil separator; replace belts; inspect check valve and minimum pressure valve; clean coolers | 2–3 hrs |
| 8,000 hours | All 4,000-hour items plus intake valve kit, thermostatic valve, safety relief valves, motor bearing inspection and relubrication | 4–6 hrs |
Oil and Filter Change (2,000-Hour Service)
Run 10–15 minutes to bring oil to operating temperature.
Shut down, disconnect power, lock out/tag out, verify zero energy, and depressurize through the blowdown valve.
Drain the separator tank into a 5+ gallon pan for 15–20 minutes, plus the airend plug where fitted.
Remove the oil filter, film the new gasket with fresh oil, and install hand-tight plus 1/2–3/4 turn—wrench-tightening distorts the gasket.
Refill to the sight glass midpoint; typical capacity 1–5 gallons.
Start, run 30 seconds, stop, and recheck: the level falls as airend, cooler, and lines fill. Top off without overfilling, since foam carries oil downstream. Recycle the used oil.
Air/Oil Separator Replacement (4,000-Hour Service)
The separator returns oil to the system while passing clean air downstream. A clogged element raises differential pressure and energy use; a failed one dumps gallons of oil into dryers, tools, and processes. Depressurize fully, remove the tank cover noting bolt positions, extract the element noting seal orientation, clean sludge from the housing, fit the new element from the air filter, oil filter & oil separator kit with new lightly oiled seals, and torque cover bolts evenly—15–25 ft-lbs on smaller machines. After restart, check the cover gasket, the commonest post-service leak point. Expect about 4,000 hours, less on a hot-running machine.
Cooling System and Ventilation
Air-cooled cooler: every 500 hours or monthly, blow compressed air through the fins from the fan side—opposite normal airflow—and straighten bent fins with a fin comb. In extreme dirt use mild detergent and low-pressure water, then dry.
Thermostatic valve: it bypasses the cooler during warm-up and routes oil through it when hot. Stuck open gives long warm-up and moisture; stuck closed gives overheating. Test annually—oil should hold 175–195°F.
Room ventilation: at least 500 CFM per 10 HP, so a 30 HP machine needs 1,500 CFM; recirculated hot discharge air is a leading cause of high-temperature trips.
Oil Analysis
For continuous duty, a $25 oil sample is the best-value tool available: it flags bearing wear (iron, copper, aluminum), dust ingestion (silicon), oil degradation (viscosity shift, rising acid number), and coolant leakage (sodium, glycol). Sample every 500 hours for the first 1,000 to build a baseline, then at each oil change; a verified program can stretch intervals past 4,000 hours.
Rotary Screw FAQ
How long does an airend last? 20,000–40,000+ hours before overhaul (bearings, rotor re-coating if damaged)—five to ten years at 4,000 hours annually. Contaminated oil, dust through a neglected inlet filter, oil starvation, and sustained outlet temperature above 200°F shorten it sharply. HPDMC's PM VSD rotary screw compressors are designed for 20,000+ hour airend life.
What are the early warning signs? Rising oil consumption (separator or seal leakage); discharge temperature creeping 5–10°F over weeks (cooler fouling, thermostatic valve) or jumping suddenly (oil starvation, airend damage); a changed whine—grinding, knocking, screeching; oil in downstream air; longer load times. A $500 repair now beats a $5,000+ airend later.
Does VSD change the plan? Slightly. Service cabinet ventilation filters every 500–1,000 hours to keep cool clean air at the electronics. Soft starting extends bearing life, but prolonged running below roughly 30% of maximum speed can starve some designs of oil. More on VSD technology.
11. Scroll Air Compressor Maintenance
Scroll compressors need a different plan because of the mechanism: no oil in the compression chamber, no metal-to-metal contact between elements, and wear concentrated in a few predictable parts. There is no oil to change and no valves or rings to rebuild—but tip seals wear and elements have finite life.
What Wears—and What Does Not
1) Tip seals. Thin self-lubricating polymer strips in the scroll wrap tips seal the orbiting and fixed scrolls. Designed to wear, they are the most frequent replacement item: about 10,000 hours, cut short by continuous discharge above 200°F, dusty intake, and frequent cycling. The first symptom is falling CFM at a given pressure; replacement runs $500–$1,200 per set.
2) Scroll elements. The matched scrolls last roughly 20,000–30,000 hours before profile erosion increases internal leakage. They cannot be repaired, only replaced as a set ($2,000–$5,000 plus labor). Budget $0.10–$0.20 per operating hour—planned end-of-life, not surprise failure.
3) Bearings. The orbiting scroll's main bearings are grease-lubricated and sealed, good for 30,000–40,000 hours. Failure announces itself as growling or rumbling plus vibration.
4) Non-wear items. No piston rings, cylinder walls, valves, rod bearings, or crankshaft seals—which is why routine maintenance frequency is lower than a piston machine.
Scroll Maintenance Schedule
| Interval | Task | Who | Time |
|---|---|---|---|
| Daily | Visual, sound, controller readings, drain | Operator | 5 min |
| Weekly | Enclosure, airflow, vibration, hour meter | Operator | 10 min |
| Monthly | Intake filter, connections, coupling, safety test, cooler fins | Tech | 30 min |
| Quarterly | Drain service, vibration measurement, hoses | Tech | 45 min |
| Annually | Filters, tip seal inspection, bearing lube, calibration, functional test | Qualified tech | 2–4 hrs |
| 10,000 hours | Tip seal replacement if not done annually | Qualified tech | 3–6 hrs |
| 20,000–30,000 hours | Scroll element replacement | Qualified tech | 4–8 hrs |
A few specifics the table cannot carry: wipe panels with a dry cloth rather than blowing dust with compressed air, which drives it into terminals and bearings; never clean paper filter media with air, since $20–$50 elements are cheap insurance against dust-driven wear; log pressure, temperature, and alarms daily, because a slow temperature rise points to tip seal wear or cooling fouling.
Annual Service
Two to four hours by a qualified technician: replace the intake filter regardless of appearance, as dirty air is the leading cause of premature element wear; inspect tip seals; purge and replenish bearing grease where fittings exist, never over-greasing; calibrate pressure sensors against a gauge, since a sensor 5 PSI high delivers 5 PSI low; torque-check terminals; replace the controller battery; and functionally test start, load, rated pressure, unload, shutdown, and alarms.
Tip Seal Inspection
■ Lock out power, remove enclosure panels, and disconnect the discharge line and instrumentation from the fixed scroll.
■ Remove the fixed scroll bolts, marking them where a tightening sequence applies, and lift the scroll off squarely—no pry bars on precision surfaces.
■ Measure seal projection above the scroll surface with a depth micrometer or feeler gauge; minimum is typically 0.5–1.0 mm.
■ Replace all seals if any one is under minimum, since partial replacement seals unevenly.
■ Clean with lint-free cloth and isopropyl alcohol—never abrasives or scrapers, as surface finish controls sealing—and reassemble with new gaskets and O-rings, torqued in sequence.
Replace the elements at the stated life, or earlier when CFM has dropped 15–20% at the same pressure, specific power has risen 10–15%, or inspection shows scoring or pitting.
Low CFM: clogged intake filter, worn tip seals, worn elements, leaking check valve. Noise or vibration: worn bearings, failing coupling, loose mounts, debris in the fan. High discharge temperature: restricted airflow, clogged filter, recirculation through tip seals, ambient above 104°F/40°C. Will not start: tripped breaker, unreset high-temperature shutdown, low supply voltage, failed controller or contactor.
12. Paintball / PCP Compressor Maintenance
Most high-pressure failures come from neglected oil, clogged filters, moisture in intercoolers, and deferred valve service—all preventable, and all caught by the routine below.
Discipline must be stricter because the duty is harsher. At 3,000–4,500 PSI every seal, gasket, and valve sees 20–30 times shop pressure, so defects harmless at 150 PSI become real leaks, and a four-stage machine carries four pistons, four valve sets, three intercoolers, and three moisture separators. Water droplets at these pressures act almost abrasively on valve seats and seals, so inter-stage moisture removal must work continuously.
Daily (5–10 Minutes)
1) Check crankcase oil at the sight glass with the machine off and cool; a falling level means a leak to find.
2) Inspect compressor, intercoolers, separators, and high-pressure piping for oil or air residue at fittings.
3) Drain all inter-stage and final separators, or verify automatic drains are cycling—no water suggests a clog.
4) Inspect the intake filter, cleaning or replacing sooner in dust, and confirm the cooling fan runs with clear airflow; a dead fan must be fixed before further running.
5) Listen at startup for knock, rattle, or hiss, and log hour meter, stage pressures, and discharge temperature—trends are the earliest warning.
Weekly, Monthly, and Quarterly
Weekly: clean dust from machine, intercoolers, and motor, since dust insulates hot surfaces; inspect high-pressure hoses for cracks, abrasion, and bulges—a hose failure at 4,500 PSI is a safety hazard; check belt tension; test shutdown functions.
Monthly (25–50 hours): change compressor oil every 50 hours or monthly in season, using only the manufacturer's high-pressure oil, drained warm, and read the used oil—metallic particles, milkiness, or black color each point to a problem. Clean or replace the intake element, blow the intercooler fins, and torque motor, pump, head, and manifold fasteners.
Quarterly (100–200 hours): replace the intake element regardless of appearance; inspect first- and second-stage valves for carbon, pitted seats, and cracked reeds, cleaning with approved solvent and never a wire brush that scratches seats; strip and clean all separators and drain orifices, since a sticking drain is the leading cause of moisture damage; replace or regenerate desiccant; and check rings through the head—first-stage ring wear costs the most CFM.
Annual Overhaul (500–1,000 Hours or End of Season)
1) Replace all intake and discharge valves on every stage: they are the highest-wear parts, and a $200–$500 set costs far less than the damage from a failure.
2) Replace all piston rings—even serviceable-looking rings have lost tension after 500+ hours at pressure—and every gasket and O-ring disturbed, since reused gaskets leak at high pressure.
3) Drain, flush the crankcase with a little fresh oil, and refill with clean high-pressure oil.
4) Inspect cylinder bores; light honing restores finish, deep scoring needs replacement.
5) Replace all high-pressure hoses, pump to cascade and fill whips, every 2 years or 1,000 hours; they degrade internally while looking fine outside.
6) Replace purification cartridges even on paintball-only machines, to stop bacterial growth in stagnant media.
7) Calibrate every gauge and transducer; a gauge 200 PSI low invites over-pressurizing cylinders.
Engine and Off-Season Care
Service a gas-engine field unit alongside the pump: oil every 50 hours, air filter cleaned every 25 and replaced every 100 (sooner in dust), spark plug inspected at 100 hours and replaced at 200, fuel filter at 200 hours or annually, stabilizer before the off-season, and a trickle charger on starting batteries.
Before storage, finish the annual overhaul first—used oil acids, separator moisture, and aged seals all deteriorate on the shelf. Drain every separator and intercooler, refill with fresh oil, cap intake and discharge openings, hold cascade pressure near 500 PSI, remove the battery, and store dry; in unheated rooms remove all water, or freezing cracks tubes and castings.
To return after three months idle: change oil showing moisture or varnish, fit a new intake filter, rotate the pump by hand where provided, run unloaded 5 minutes, then load gradually while watching stage pressures and temperatures. Soap-check connections and verify shutdown protections before the first fill.
13. Engine-Driven Compressor Maintenance
The engine is the heart of a portable unit—Kohler-powered or Lonxin—and engine neglect means missed deadlines and avoidable repairs. Five habits cover most of it. We covered the selection side in our earlier gas-powered air compressor buying guide.
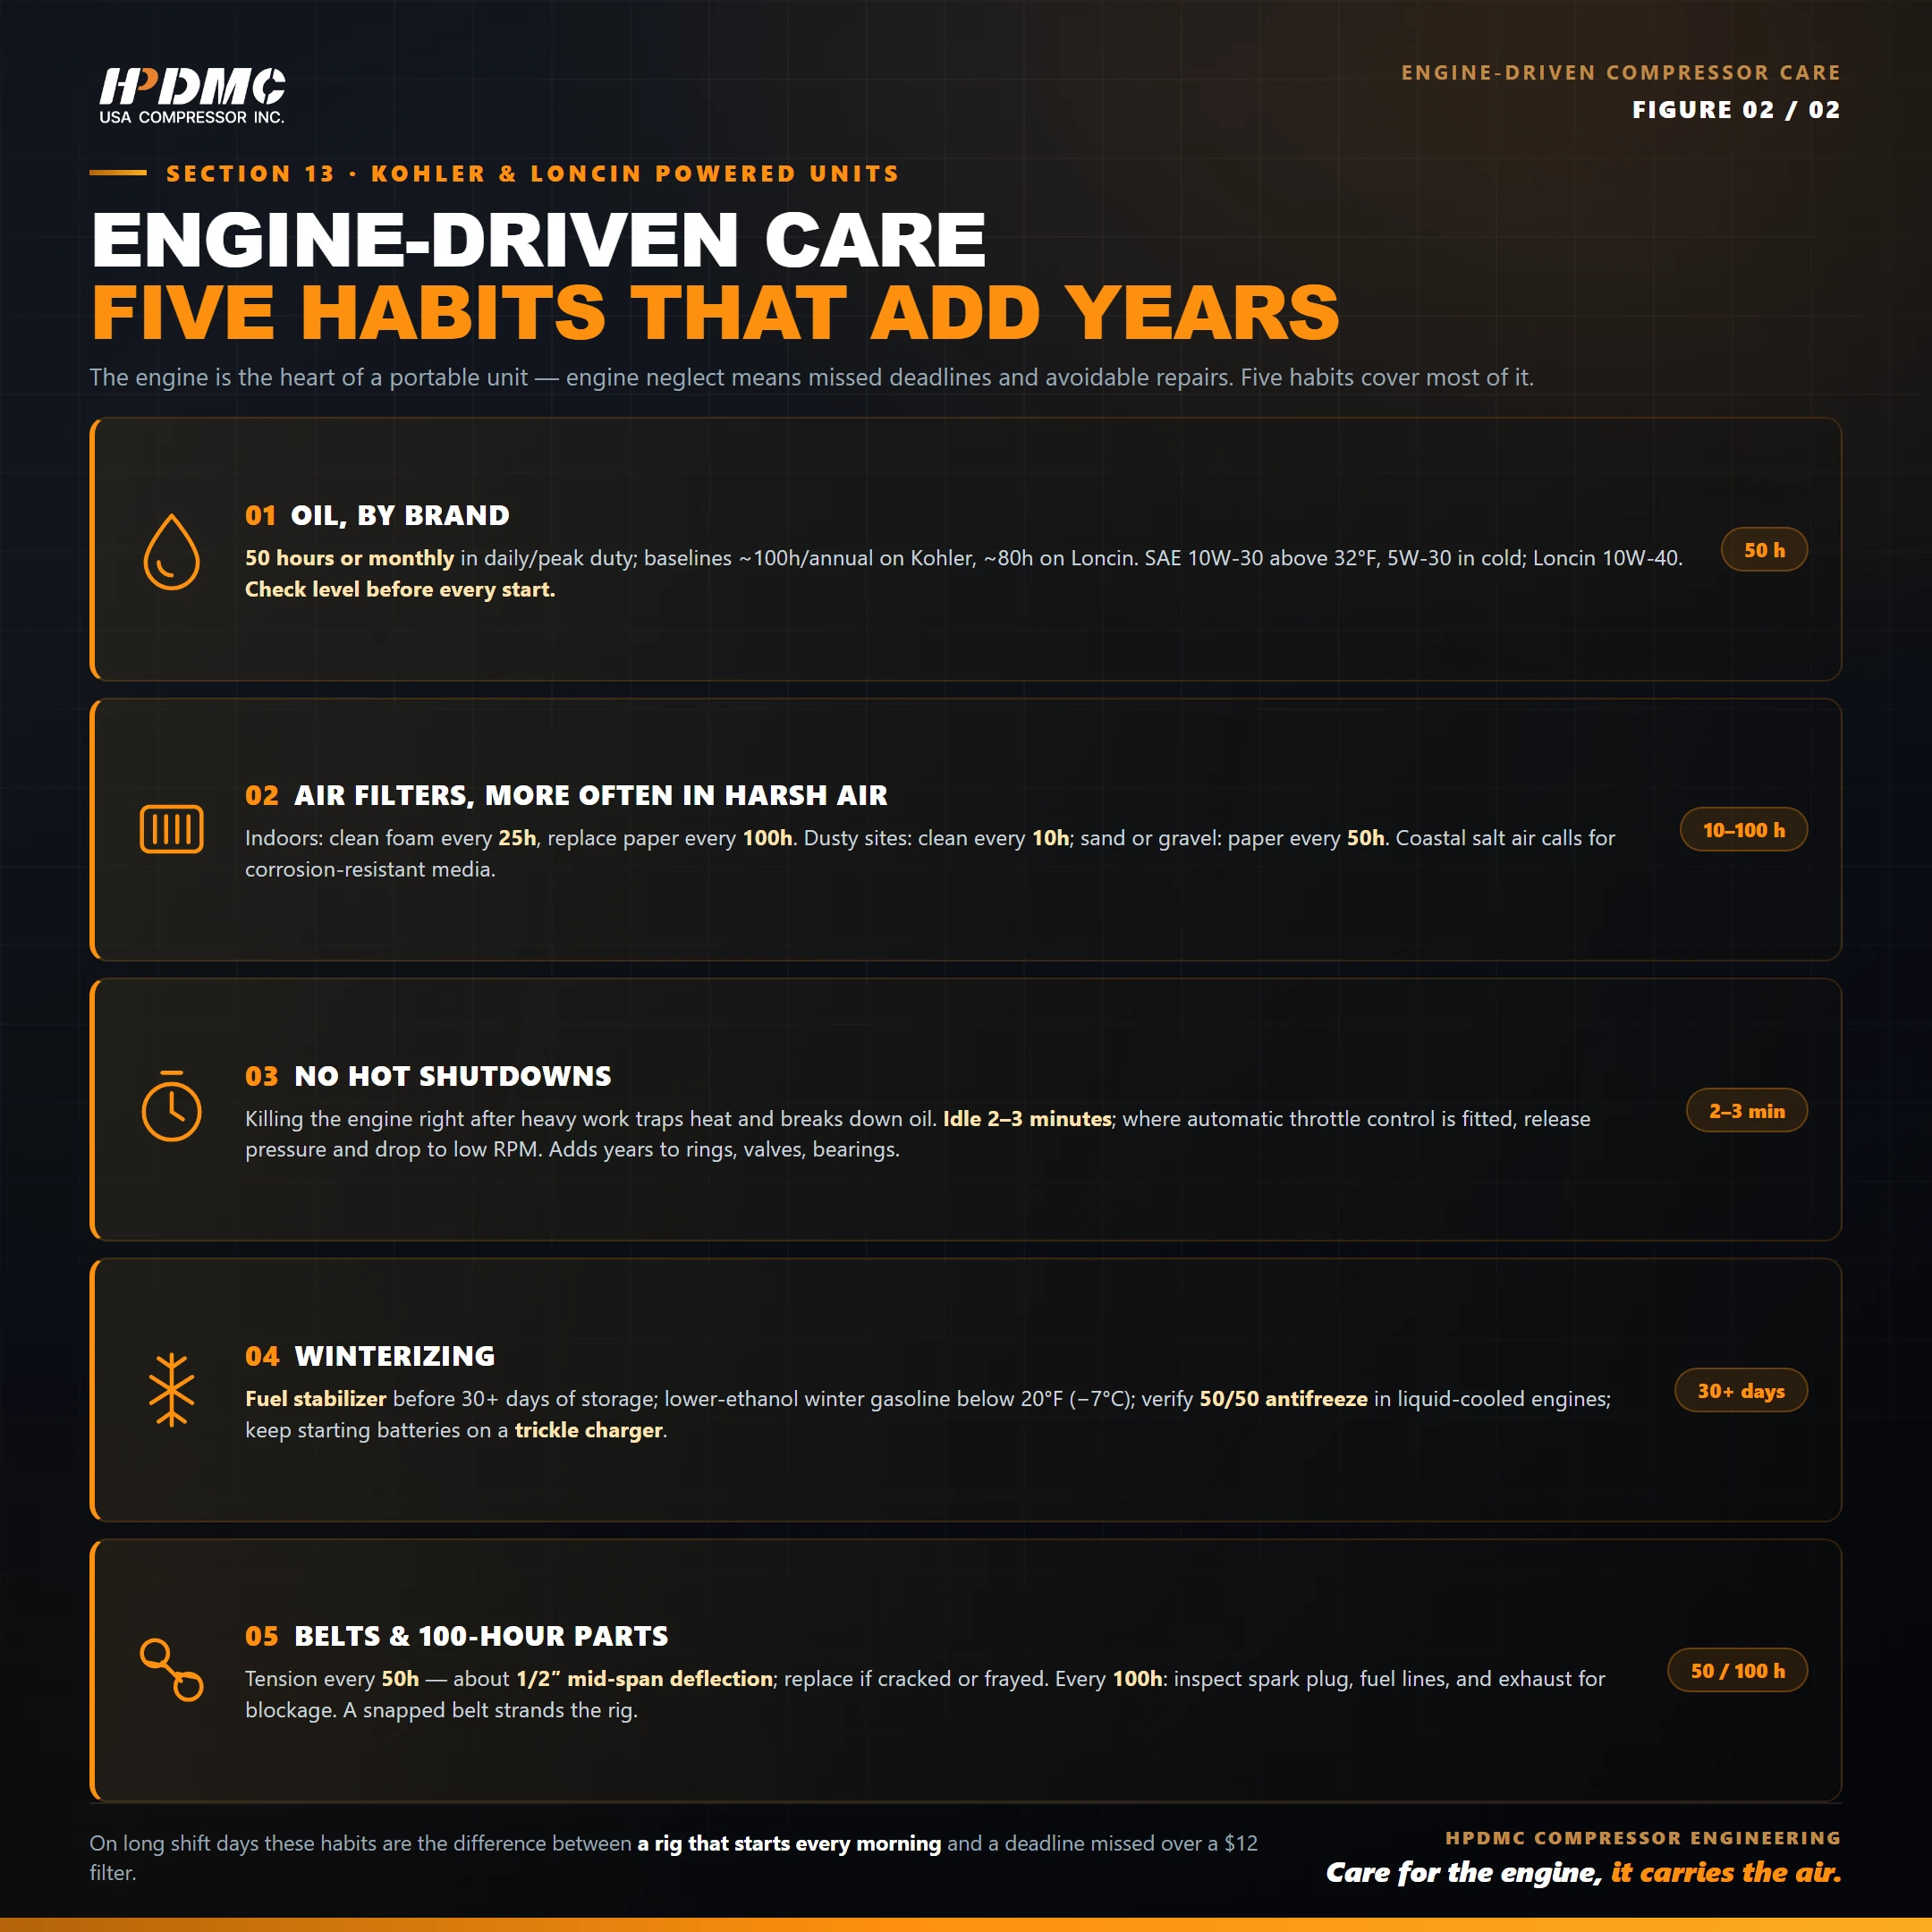
Oil, by brand. For daily or peak-season duty change engine oil every 50 hours or monthly; brand baselines run roughly 100 hours or annually on Kohler and about 80 hours on higher-compression Lonxin engines. On the HPDMC 6.5HP portable gasoline compressor with Kohler engine, use SAE 10W-30 above 32°F (0°C) and SAE 5W-30 in cold climates; Lonxin units suit high-quality detergent oil, typically SAE 10W-40. Check the level before every start—low oil destroys an engine fast.
Air filters, more often in harsh air. Indoors, clean foam elements every 25 hours and replace paper every 100. On dry dusty sites clean every 10 hours, and on sand or gravel replace paper every 50. Coastal salt air calls for corrosion-resistant media.
No hot shutdowns. Killing the engine right after heavy work traps heat, breaks down oil, and loads valves and gaskets. Idle 2–3 minutes so temperatures fall gradually; where automatic throttle control is fitted, release pressure and let it drop to low RPM. On long shift days this habit adds years to rings, valves, and bearings.
Winterizing. Add stabilizer before 30-plus days of storage, use lower-ethanol winter gasoline below 20°F (−7°C), verify a 50/50 antifreeze mix in liquid-cooled engines, and keep starting batteries on a trickle charger, since cold cuts capacity.
Belts and 100-hour parts. Check tension every 50 hours—about 1/2" (1.27 cm) of deflection at mid-span under moderate pressure—adjust if loose, replace if cracked or frayed; a snapped belt strands the rig. Every 100 hours inspect the plug, fuel lines, and the exhaust for blockage.
14. Why Maintenance Matters
Neglect surfaces three ways. Energy costs climb, because a dirty filter or worn belt cuts efficiency by 10–30% as the machine works harder for the same air. Failures arrive early, since a rusted tank or burned motor costs thousands. Safety erodes, as over-pressurized tanks and faulty valves can rupture and a damaged panel creates fire and electrocution hazards.
15. Frequently Asked Questions About Air Compressor Maintenance
How often should I change my air compressor oil?
Pump oil every 300 operating hours or annually, whichever comes first, cut to 200 hours in dust or heat; gas engine oil every 50 hours or monthly. The break-in change—first 50 hours on a pump, first 5–8 on an engine—is the most critical, clearing manufacturing debris. Use non-detergent mineral compressor oil, ISO 100 or SAE 30.
What happens if I don't drain my compressor tank?
Water at the bottom forms a corrosion cell that thins the shell from the inside, invisibly, until it fails. It also cuts usable volume, breeds bacteria whose acidic byproducts speed corrosion, and rusts tools from within. Daily draining can add decades of tank life; where it is impractical, an automatic tank drain at $40–$80 pays for itself.
Can I use automotive oil in my compressor pump?
No. Automotive oil holds detergents and dispersants meant to suspend combustion byproducts. In a pump that runs hot and clean, those additives break into carbon on the valves, causing sticking, lost compression, and valve failure. Use non-detergent mineral compressor oil (ISO 100 or SAE 30); see the oil selection guide.
What oil do high-pressure paintball and PCP compressors use?
Synthetic or semi-synthetic oil formulated for high-pressure reciprocating service, commonly ISO VG 100 or 150, with high oxidation stability and strong water separation. Never automotive oil, hydraulic oil, or oil rated only for 150 PSI duty.
How do I know when a belt needs replacing?
Replace on cracking inside the rib, glazing (a shiny, hardened surface that means slipping), edge fraying, uneven wear, or when tension adjustment is exhausted. Preventively, replace every 2–3 years, as rubber degrades silently, and keep a spare.
My compressor sat unused for months. What now?
Change pump oil if milky or varnished, drain the tank completely, and on gas models drain old fuel, fit a fresh plug, and confirm the filter is clear. Rotate the pump by hand to prove free movement, then start with the tank drain open for 30 seconds to circulate oil before building pressure.
Why won't my compressor reach full pressure?
Work stage by stage. On piston and high-pressure machines the usual order is worn rings, leaking or sticking valves, a clogged intake filter, leaking inter-stage joints or separator drains, then worn bores. On scroll units expect a clogged filter, worn tip seals, worn elements, or a leaking check valve.
Do rotary screw compressors need different maintenance than piston?
Yes. Use only manufacturer-specified rotary screw oil; run 2,000–4,000 hour oil intervals instead of 300; replace air/oil separator elements on the same cycle; and treat the inlet filter as critical, since one dust ingestion event scores precision rotors. Full procedures are in our rotary screw maintenance guide.
Do scroll compressors need oil changes?
No. The compression chamber runs dry, so there is no compressor oil to change. Only motor bearings may need periodic greasing where fittings exist; sealed bearings need none.
Can I do this maintenance myself?
Daily and weekly work—oil level, condensate drain, visual and sound checks—is operator territory after brief training. The 500-hour, monthly, and quarterly tasks need mechanical competence and the service manual; annual overhauls, tip seal inspection, and high-pressure valve and ring work belong to a qualified technician, while the HPDMC news center has more air compressor guides.


Find the Right Compressor for Your Needs
Find the Right Compressor for Your Needs